As a plastic profiles machine supplier, I’ve spent the last 12 years talking to factory foremen, line leads, and frontline workers who’ve seen firsthand what happens when safety slips around these workhorses. I’ve stood on production floors where a half-unlocked guard on an extruder led to a mangled sleeve, and heard from crews who had to shut down a full shift because a pressure relief valve wasn’t tested before a run. This job isn’t just about selling machines—it’s about making sure the people running them go home to their families every night. Let’s break down the practical, day-to-day steps we (as equipment providers, trainers, and partners) take to keep those workers safe, no matter how long their shift is or how tight their production deadline is. Plastic Profiles Machine
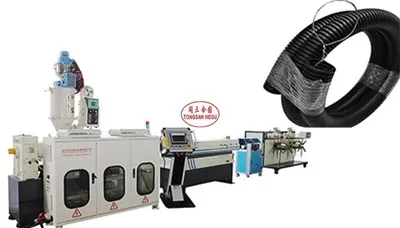
First, let’s start with the basics that most suppliers and factories skip after installation: equipment-specific safety features that aren’t just “standard” but tailored to plastic profiles machines. When we design or build these lines, we don’t just add guards as an afterthought—we build them into the machine’s core. For example, most modern plastic profiles machines have rotating extruder screws that are responsible for melting and shaping plastic resin; exposing those screws is not only inefficient (it can cause inconsistent profile shapes) but extremely dangerous. That’s why our machines use interlocking, pressure-sensitive guards for the extruder throat and the haul-off unit, which pulls the finished profile after it’s shaped. The guard won’t let the machine start if it’s not fully closed, and if someone opens it mid-run (for a jam, for example), the entire line shuts down in less than a second—no more reaching in for a hot, spinning screw.
But here’s the thing: safety features only work if they’re used. We’ve seen factories take guards off to speed up changeovers, or disable interlocks because they delay production, and that’s where 70% of incidents around plastic profiles machines happen, per OSHA data. That’s why our team doesn’t just drop a machine at a factory and leave—we work with their lead technicians to map every guard, interlock, and emergency stop (E-stop) button, and we do it on their floor, not in a training room. We’ve seen factories label E-stops with neon tape, but we remind them to test every single one every shift, not just once a month. Last year, a client in Ohio told us that their night shift team had an E-stop button that was covered in plastic dust, so when a worker noticed a jam in the cutter, they couldn’t find it fast enough. We worked with their team to create a routine: before every shift, one designated person tests all E-stops, cleans any dust off exposed buttons, and signs off on a safety checklist. Simple, but it stopped that problem cold.
Next, personal protective equipment (PPE) isn’t a “one-size-fits-all” rule we send in a pamphlet. Plastic profiles machines run hot—extruder zones can reach 400 degrees Fahrenheit, so hot plastic can spit or drip if a line jams, and haul-off rollers can run at 100 feet per minute, enough to pull loose clothing or hair in seconds. We tell every client that PPE for their line workers needs to cover specific risks, not just generic hard hats. For example, we recommend flame-resistant (FR) coveralls, not cotton or polyester shirts, because hot plastic splatters will melt cotton but slide off FR material; steel-toe boots with a non-slip sole to prevent slips on resin dust or water used to cool profiles; and face shields that cover the entire face, not just safety glasses, because even a small piece of flying plastic can scratch an eye or cause a worse injury. We also work with factories to ban loose jewelry, long hair that isn’t tied back under a hard hat, and baggy sleeves—we’ve had too many workers get their watch caught in a haul-off roller because they thought it was fine to wear for a 12-hour shift.
Another big, often overlooked risk around plastic profiles machines is plastic dust and fumes. When you’re running lines 24/7, resin dust (from PVC, HDPE, or other plastics) builds up on machinery, floors, and even air vents. In high concentrations, this dust is flammable—PVC dust, for example, has a lower explosion limit of about 20 grams per cubic meter of air, which is a lot less than many factories realize. Not only that, but the fumes from melted plastic can irritate lungs and cause long-term respiratory issues for workers who breathe them in all day. That’s why our machines come standard with integrated dust extraction systems that pull dust from the hopper and cutter sections before it can build up, and we also recommend local exhaust ventilation (LEV) for the extruder cooling zone to pull fumes away from the operator. We train teams to clean dust off machine surfaces every shift, not just once a week, and we even help them set up a simple schedule for testing dust levels—using a cheap handheld monitor that costs less than $500, something most small factories can afford.
Then there’s routine maintenance and training, which go hand in hand. A plastic profiles machine is like a car—if you skip an oil change, it breaks down, but if you skip checking pressure relief valves or extruder screw alignment, it can cause serious injury. We don’t just send a 20-page maintenance manual and call it a day; we offer on-site training for the lead maintenance team, and monthly check-ins over the first year of machine use to make sure they’re following the right procedures. For example, the extruder’s pressure relief valve is designed to release excess pressure if the screw gets jammed, preventing the machine from blowing up. We’ve seen a factory forget to test this valve for six months, and when a jam happened, pressure built up and caused a small explosion that hit a worker’s arm. We teach teams to test pressure relief valves every time they do a line changeover, not just during annual overhauls.
Training isn’t just for maintenance either—new hires on the line often get put to work fast because factories are short-staffed, and that’s when mistakes happen. We work with factories to create a “buddy system” for new workers: every new hire spends their first 10 shifts with an experienced line lead, not just a 2-hour online course. We also do refreshers every quarter, because workers get used to the machine and start cutting corners. Last year, a client in Texas told us that their line lead noticed a new worker tried to bypass a guard to fix a jam, not because they were careless, but because they’d been taught to “work fast” during their first week. Our refresher training focused on that specific scenario: what to do if a jam happens, how to turn off the line properly, and why not bypassing guards is faster in the long run (fixing a jam the right way takes 2 minutes, bypassing a guard takes 2 days of downtime if you get injured).
We also emphasize the importance of shift-specific safety. Plastic profiles machines often run multiple shifts, and night shift workers can get complacent because there’s less supervision. That’s why we help factories assign a dedicated safety lead for each shift, someone who isn’t just there to check production, but to walk the floor every hour, make sure guards are in place, E-stops are working, and PPE is being worn. We’ve seen night shift teams come up with their own small safety hacks—like putting glow tape around E-stops so they’re easy to find in low light, or setting up a spot for loose tools so they don’t get caught in rollers—and we encourage them to share those ideas with other shifts. At the end of the day, the people working the line know the machine better than anyone, so their input matters more than any rule from a handbook.
One thing we always tell clients is that safety doesn’t have to slow down production. A lot of factory managers think that adding guards, testing E-stops, or cleaning dust will make their line less efficient, but the opposite is true. When workers feel safe, they’re more focused, and incidents that cause downtime (like injuries, explosions, or fires) don’t happen. Last quarter, we had a client that went six months without a single safety incident after implementing the steps we talked about, and their production rate actually went up by 8% because they didn’t have to stop for avoidable issues. That’s the win-win: keeping workers safe and keeping production running smoothly.
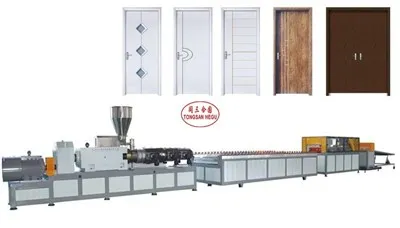
If you’re running a plastic profiles line and looking to update your machine, or want to review your current safety protocols, we’re here to help. We work with factories of all sizes, from small local operations to large national production facilities, to build machines that are safe, and to partner with your team to make sure safety stays a top priority on the floor. Reach out to us to learn more about how we can support your workers and your production goals.
References
Corrugated Box Making Machine Occupational Safety and Health Administration. (2022). Safety Guidelines for Extrusion Press Operations. U.S. Department of Labor.
National Institute for Occupational Safety and Health. (2021). Hazards of Plastic Dust and Fumes in Manufacturing Facilities. Centers for Disease Control and Prevention.
Plastics Industry Association. (2023). Best Practices for Safe Operation of Plastic Profile Extrusion Lines. Plastics Industry Association.
Qingdao Tongsanhegu Plastic Machinery Manufacturing Co., Ltd.
Address: West of Xixinzhi Village, Sanlihe District Jiaozhou, Qingdao City, Shandong Province, China
E-mail: info@tongsanhegu.com
WebSite: https://www.tongsanhegumachine.com/
